Aerogel Technologies

How Aerogel Technologies Recovered Complex Solvents with Maratek's SSBP-110 System

2019 CASE STUDY | ADVANCED MATERIALS & TEXTILES

Customer: Aerogel Technologies
Location: USA
Equipment: SSBP-110 Solvent Saver Batch Premium, 110-gallon capacity.

Aerogel production involved a challenging mixture of tert-butyl alcohol, N-methyl-2-pyrrolidone (NMP), and water. Aerogel Technologies needed dependable solvent recovery while controlling freezing risks and operating in a hazardous environment.

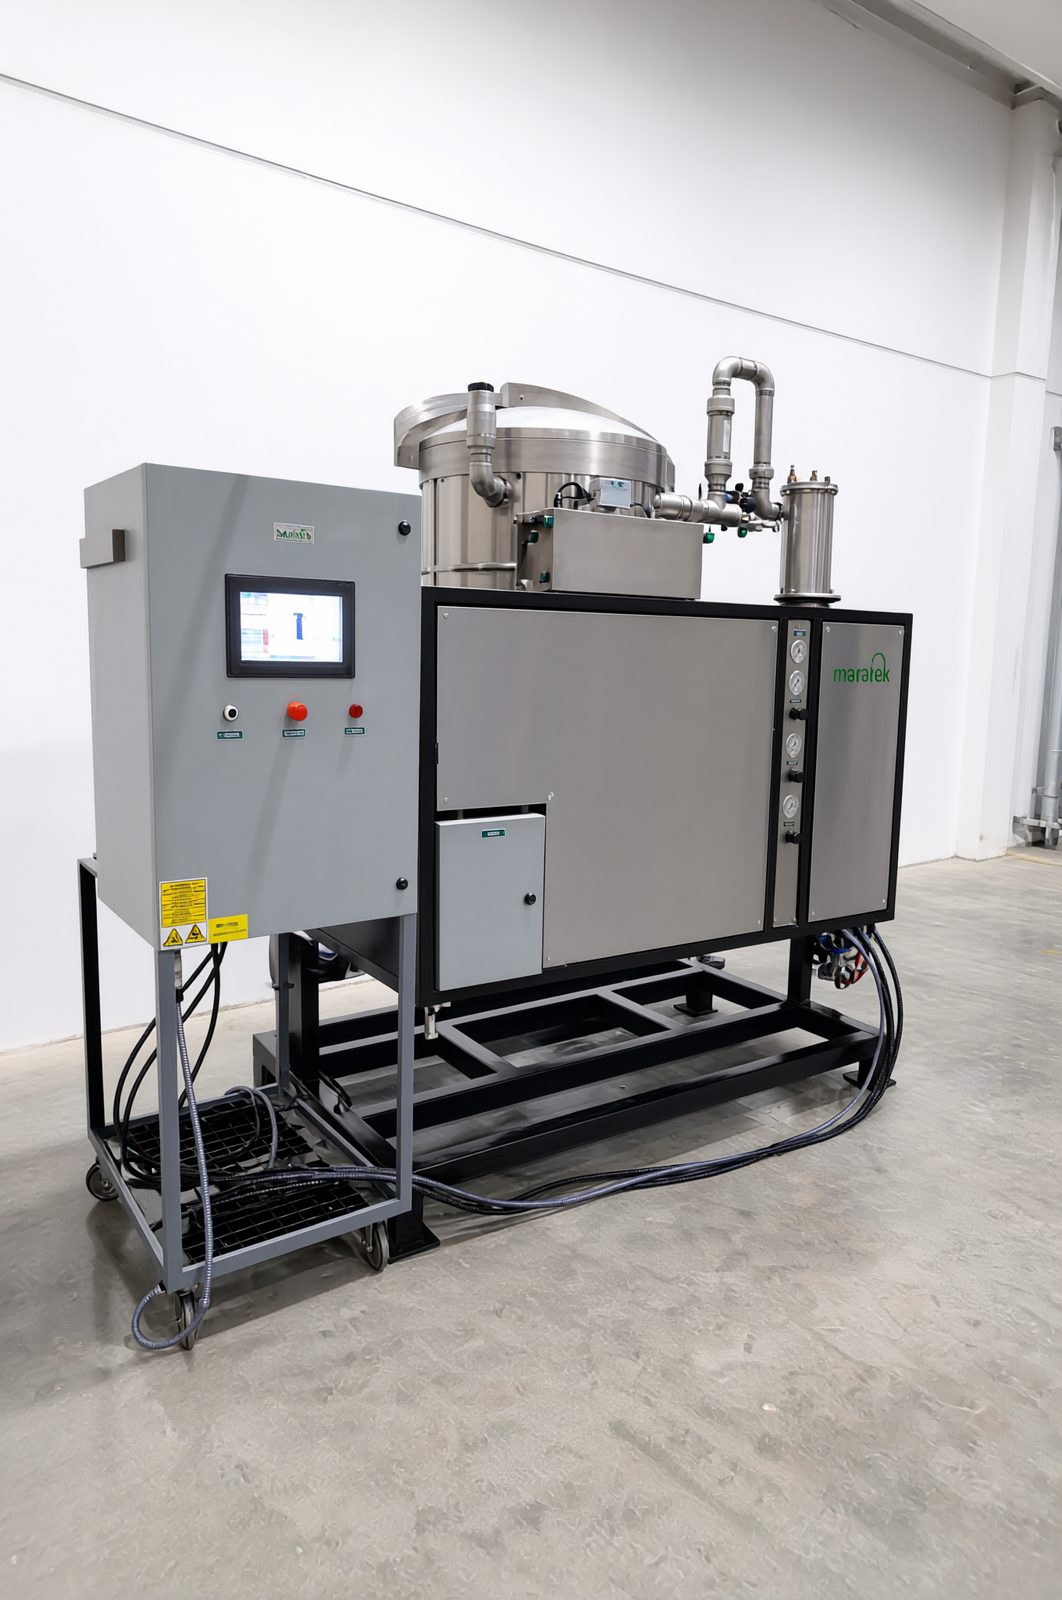
Maratek engineered and installed a customized 110-gallon SSBP-110 recovery system combining thermal oil heating, water-cooled condensation, mist elimination, dual-drum collection and remote Ethernet PLC support.

The outcome: The original case study reports efficient recovery of the mixed solvents without freezing, improved operational reliability, and support for fireproof textile development.

Maratek
Chemistry icon

110-Gallon SSBP-110 System

Solvent recovery icon

Tert-Butyl Alcohol, NMP & Water

Equipment performance icon

50°C–200°C Thermal Oil Heating

Safety specification icon

Class I, Division 1, Group D Certification

Automation icon

Remote PLC Support & Automated Collection

The Challenge: Recovering a Complex Solvent Mixture Safely

Aerogel Production Requirements

Aerogel is a very lightweight solid known for thermal insulation and flame resistance. Its production required recovery of a complex mixture of tert-butyl alcohol, NMP, and water.

The customer needed a system that could recover different solvents, prevent tert-butyl alcohol from freezing and operate safely in a hazardous environment. Traditional systems did not offer the flexibility or specified safety certification for the application.

Maratek's Tailored SSBP-110 Solution

  • Thermal oil jacket: Precise heating from 50°C to 200°C.
     
  • Water-cooled copper condenser: Recovery of volatile solvents.
  • Mist eliminator: Removal of entrained droplets to improve distillate quality.
  • Dual drum filling and collection: Reduced manual intervention.
  • Tilting frame: Easier sludge discharge and cleaning.
  • Remote Ethernet PLC: Real-time support and software updates.
  • Class I, Division 1, Group D: Certification specified in the source case study.

Optional upgrades described: A 10-ton water chiller to prevent tert-butyl alcohol freezing, a jacketed mixing vessel for molecular sieve dehydration and jacketed storage totes with spill sensors.

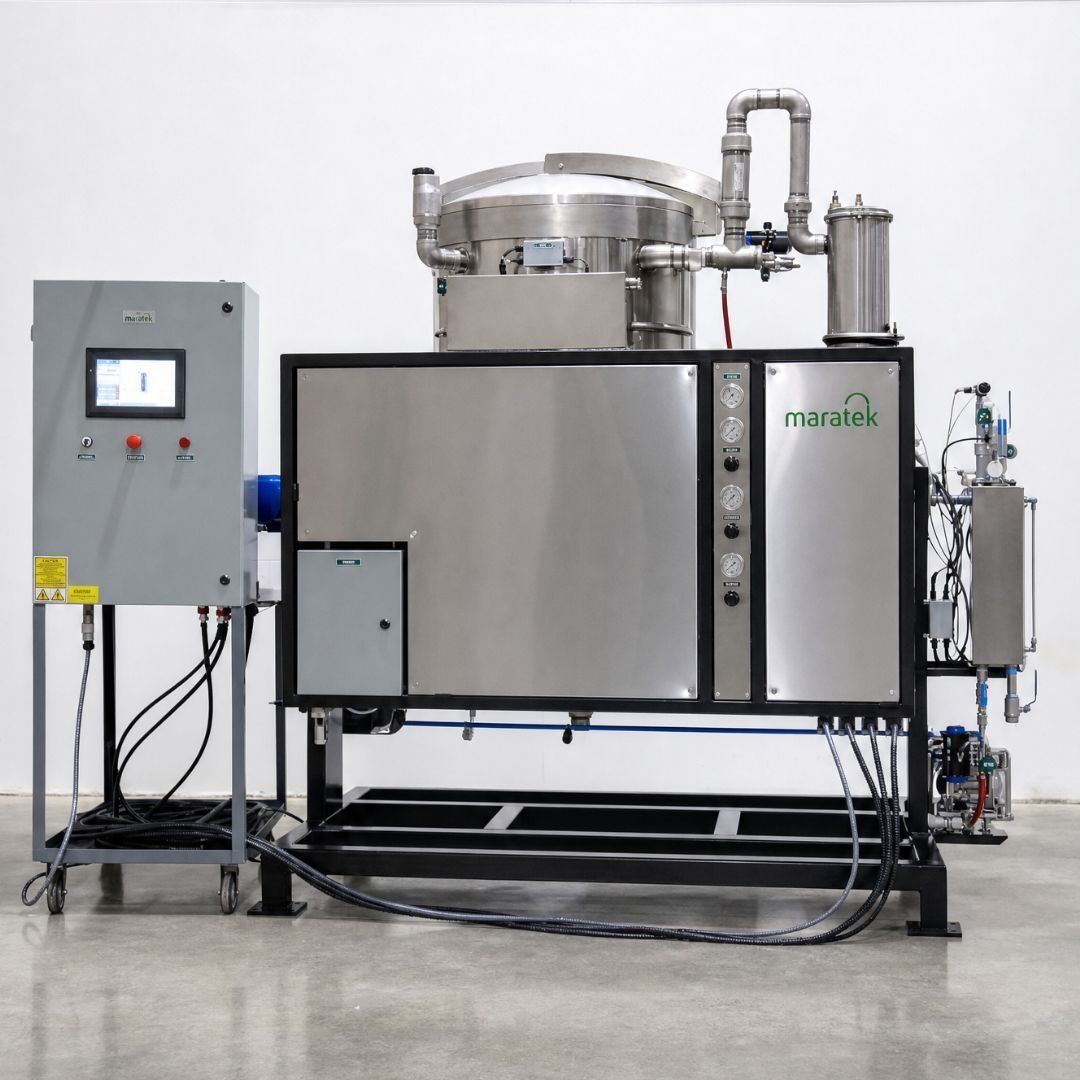
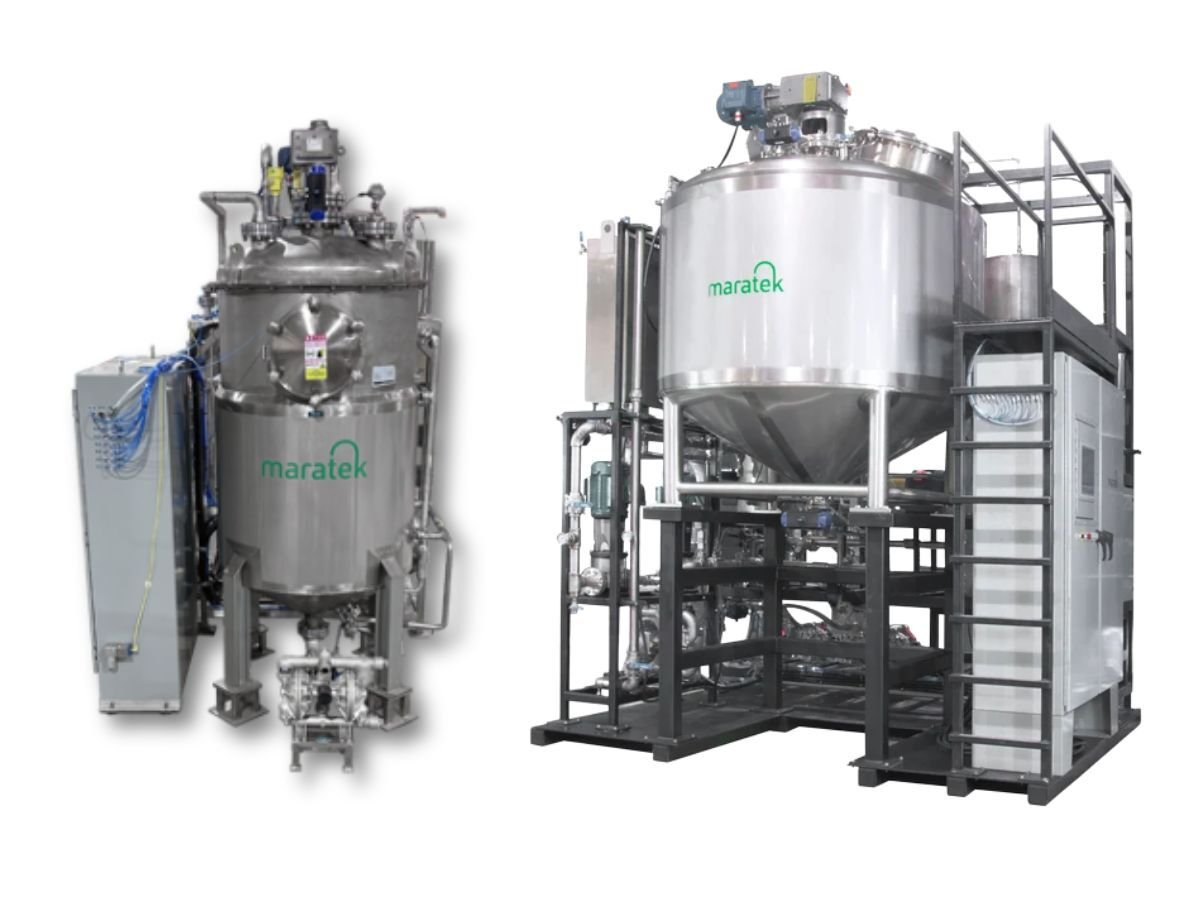
Angled view of Maratek stainless steel solvent recovery system with PLC control cabinet

The Results: Recovery, Reliability and Safety

The original 2019 case study documents four outcomes:

  • Recovery of a challenging mixture: Tert-butyl alcohol, NMP and water were recovered efficiently without freezing.
  • Process reliability: Automated collection, remote support and spill sensors reduced downtime.
  • Safety and compliance: The Class I, Division 1, Group D certification and food-grade construction addressed the project's stringent safety standards.
  • Innovation support: The system enabled Aerogel Technologies to advance development of fireproof textiles.

Find Your Payback: Three Volume Scenarios

Whether you process 1 drum a day or 6+, there's a Maratek solution.

The figures below are example scenarios for in-house solvent recovery in general, not results from the Aerogel Technologies project.

Daily Volume 1 Drum/Day 4 Drums/Day 6 Drums/Day
Monthly Gallons 1,155 gal 4,620 gal 6,930 gal
Estimated Monthly Savings $7,500 $25K–$35K $40K–$60K
Estimated Equipment Cost $75K–$90K $150K–$250K $250K–$350K
Payback Period 1 Year 6–9 Months 6–9 Months
10-Year Savings  $900,000   $3M–$4.2M   $4.8M–$7.2M 

Example results. Contact us to calculate your equipment sizing and ROI based on your operation.
Calculate My Payback

What Made the Aerogel Recovery System Different?

Three engineering requirements shaped Maratek's approach to this custom solvent recovery project.

Multi-Solvent Recovery

Designed for a process mixture containing tert-butyl alcohol, NMP and water.

Freezing Prevention

The project included an optional 10-ton water chiller intended to prevent tert-butyl alcohol freezing.

Environment Design

The equipment specification included Class I, Division 1, Group D certification and remote PLC support.

Explore Related Solvent Recovery Solutions

Learn more about Maratek's recovery equipment and engineering services.

Maratek (1)

Solvent Saver Series

Learn about Maratek's solvent saver recovery equipment.

Explore Equipment
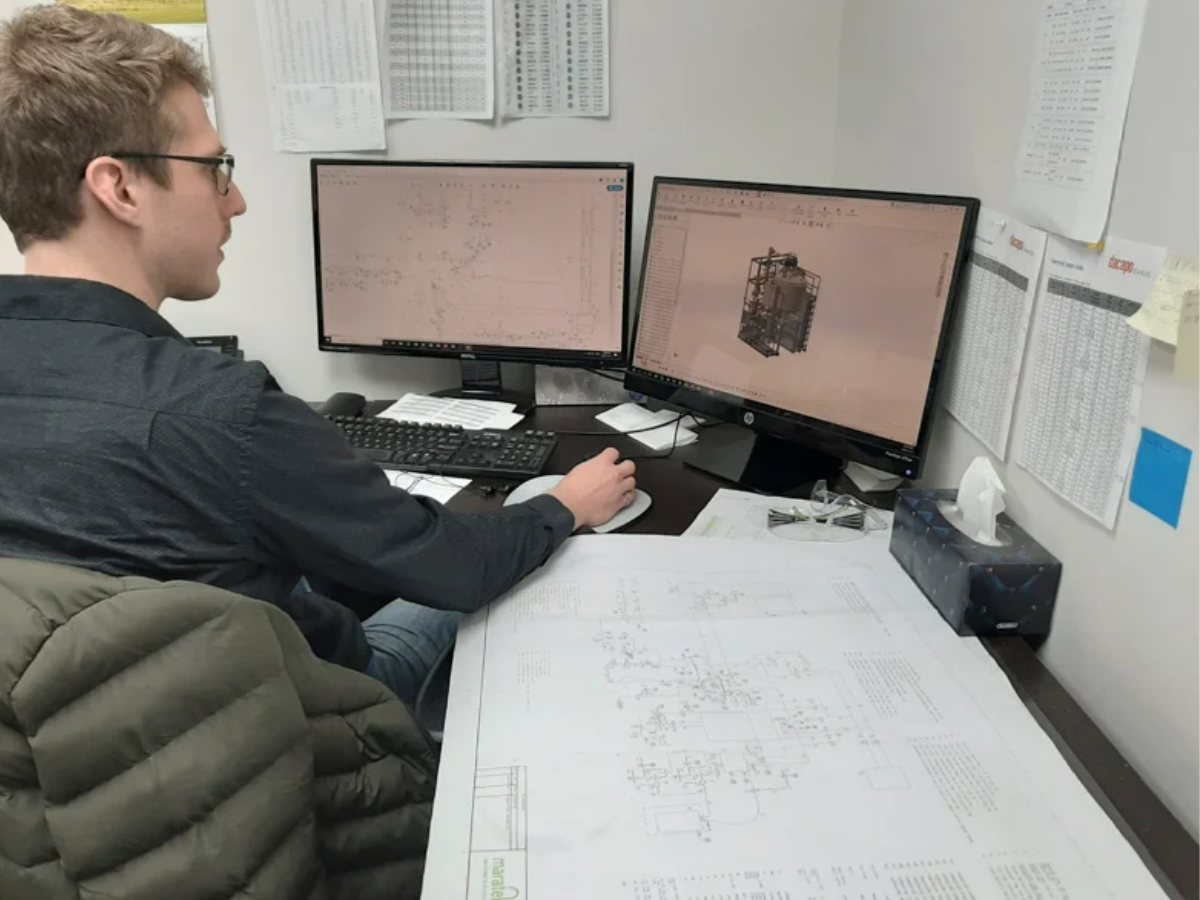
Maratek engineer designing a custom solvent recovery system in CAD

Engineered-to-Order Systems

See how custom engineering can address your specific needs.

Explore Engineering

Frequently Asked Questions

Which solvents did Aerogel Technologies need to recover?

The production process described in Maratek's 2019 case study used tert-butyl alcohol, N-methyl-2-pyrrolidone (NMP) and water.

What equipment did Maratek supply?

Maratek installed the 110-gallon SSBP-110 Solvent Saver Batch Premium System, tailored to the customer’s requirements.

How did the project address tert-butyl alcohol freezing?

The case study identifies a 10-ton water chiller as an optional upgrade designed to prevent freezing.

Which hazardous-area certification was specified?

The case study states Class I, Division 1, Group D certification.

Did the project report a solvent recovery percentage or financial ROI?

No. The published 2019 source describes qualitative results but does not provide a numerical recovery percentage or financial return.

Solvent recovery for a challenging process? Get a custom engineering quote.